Custom engineered for Commercial Organic Fertilizers, Bio-Organic Granules, and Compost Pellets. Seamless integration of aerobic fermentation, high-efficiency crushing, precision batching, rotary/disc granulation, drying, cooling, screening, and automatic packaging (1 to 20 T/h).
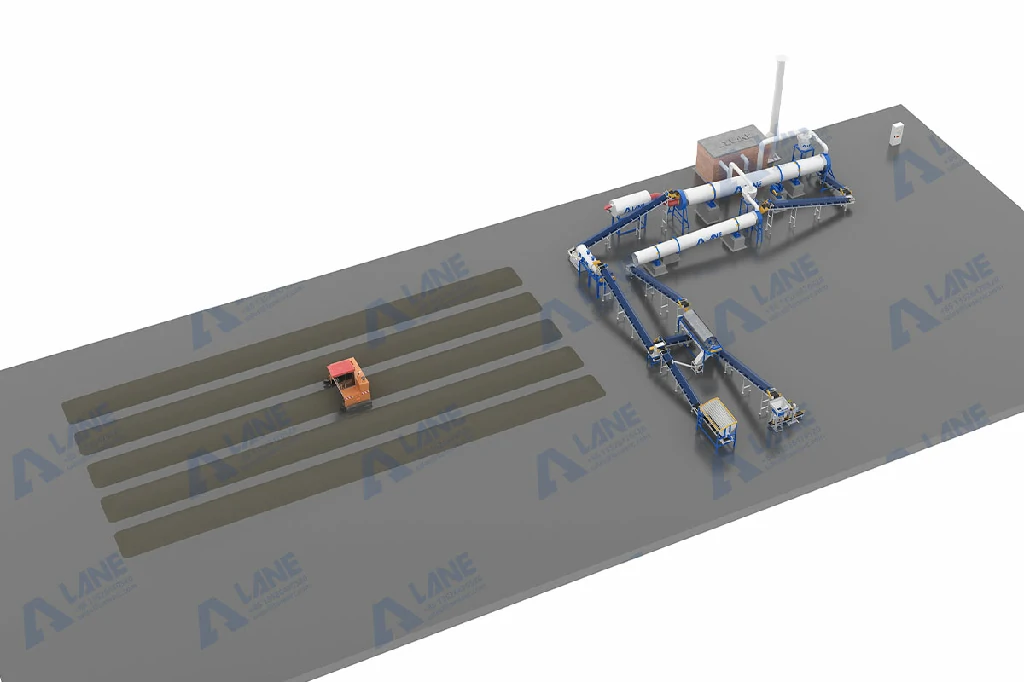
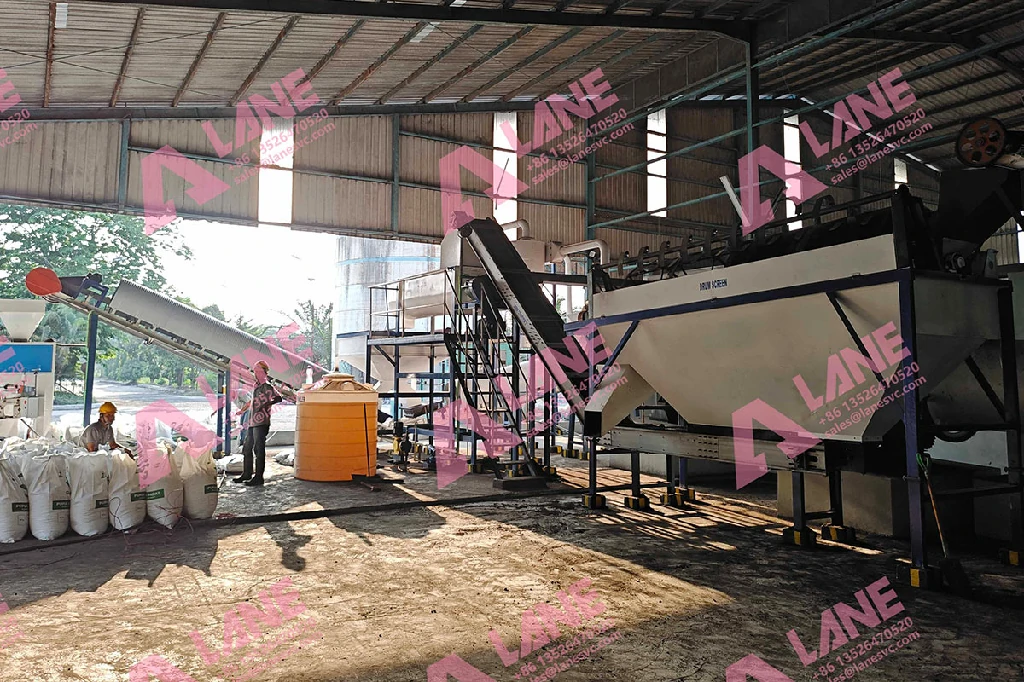
Click to Play: 5-10 T/h Commercial Organic Fertilizer Granulation & Automated Packaging Line
Select your organic raw materials, composting technology, capacity, and automation requirements to generate a real-time turnkey USD investment estimate.
Engineered with heavy-duty anti-corrosion alloys, high-torque reducers, and wear-resistant liners to handle tough organic waste and high continuous loads.
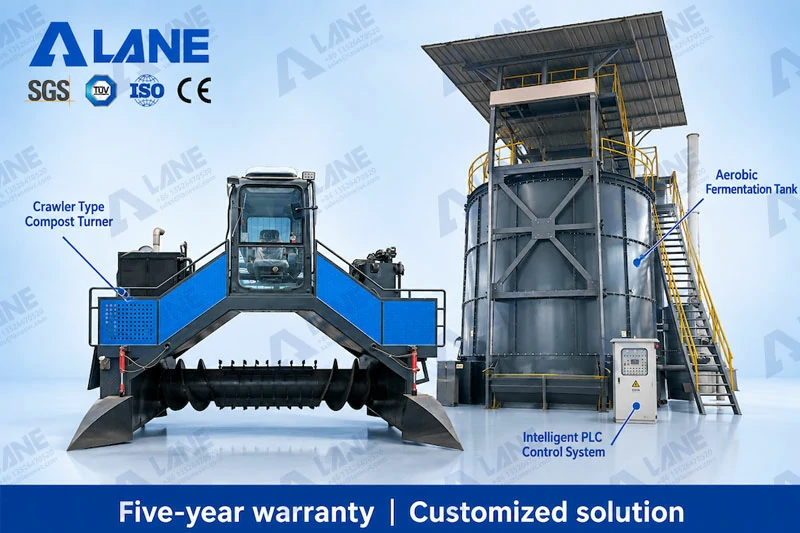 Core Unit 01
Designed for windrow composting of poultry manure, straw, and organic waste. Equipped with hydraulic lifting rotor, high-torque diesel engine, and biological inoculant sprayers.
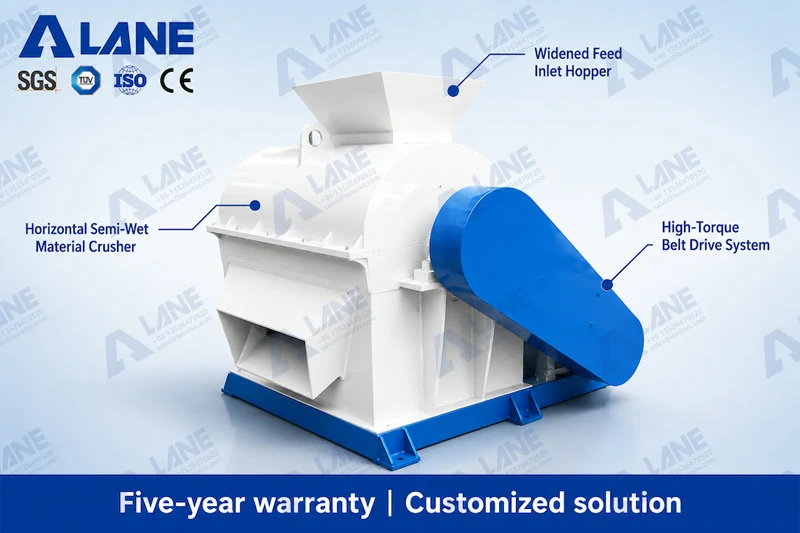 Core Unit 02
Specifically built for fermented organic materials containing 25%~50% moisture. High-strength wear-resistant alloy chain hammers completely prevent clogging and wall sticking.
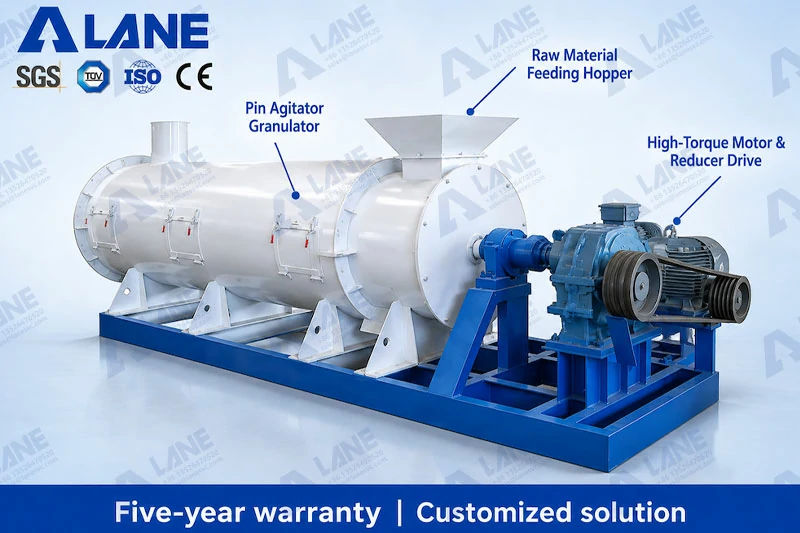 Core Unit 03
Uses high-speed rotating stirring teeth to mix, agglomerate, and granulate powder materials into uniform, compact spherical pellets. Features high granulation efficiency, strong adaptability to different raw materials, and a compact structure for continuous production.
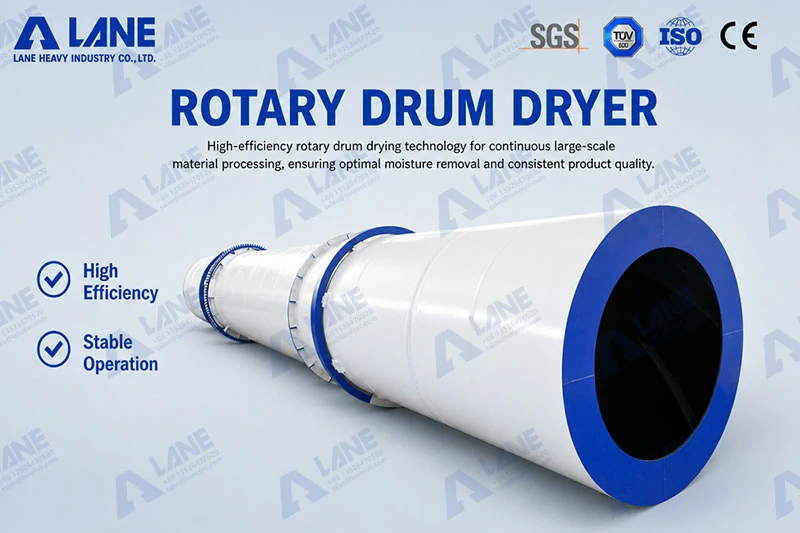 Core Unit 04
Heavy-duty counter-current rotary drum system paired with high-efficiency cyclone dust collectors and bag filters. Reduces pellet moisture from 30% down to under 12% without thermal degradation.
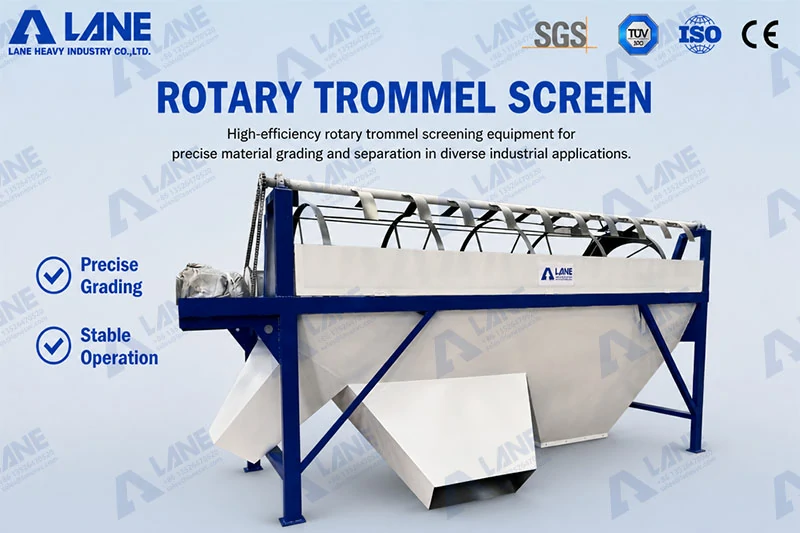 Core Unit 05
Double-layer rotary screen separates qualified pellets, oversized lumps, and fine powders. Integrated liquid/powder coating drum sprays anti-caking oil and conditioning agent for long shelf life.
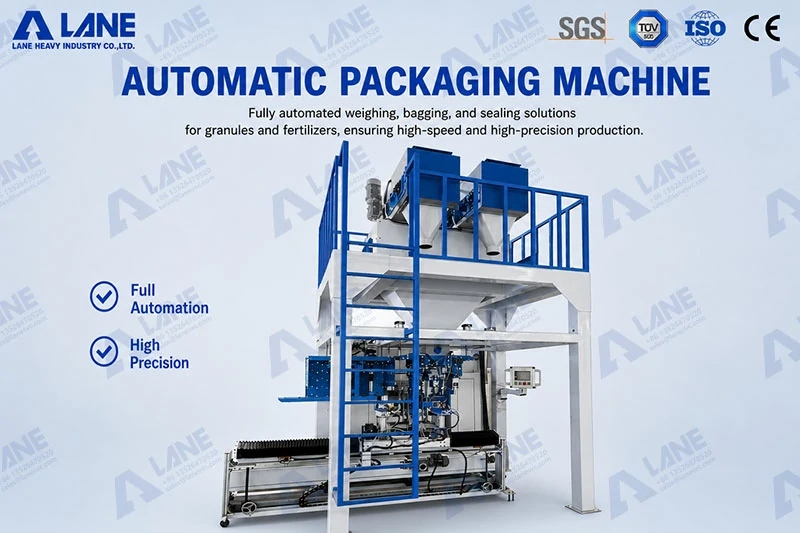 Core Unit 06
High-precision dual-weighing hopper packaging machine with auto bag clamping, thermal sealing, and sewing conveyor. Central Siemens PLC cabinet manages recipe dosing and entire plant synchronization.
From raw material testing, civil plant layout design, machinery manufacturing to overseas installation and agronomist support, we deliver complete end-to-end solutions.
Custom 2D/3D plant layout, fermentation windrow trench civil drawings, and utility planning (electricity, drainage, deodorization) optimized for your site terrain.
Our agronomist and chemical team optimizes C/N ratios, selects high-activity aerobic microbial inoculants, and provides custom organic-inorganic blend formulas.
We dispatch veteran mechanical, welding, and electrical engineers directly to your site for machinery positioning, conveyor alignment, wiring, and live trial runs.
24-month structural warranty, global client tracking, IoT remote diagnostics, and critical wear-resistant spare parts (chains, hammers, liners) express delivery within 48h.
Find answers to the most common questions regarding composting methods, granulator selection, lead times, and on-site engineering.
Windrow Composting (Turner): Suitable for open fields or rain sheds. Piles are 1.5-3m wide and turned periodically by crawler/wheel turners. Takes 15-25 days, has low equipment investment cost, and handles massive raw material volumes.
In-Vessel Aerobic Fermentation Tank: A fully enclosed vertical cylindrical reactor. Aerobic microorganisms decompose waste under automated forced aeration and temperature control (55°C-65°C). Takes only 7-10 days, occupies minimal land, and features integrated biological deodorization for strict environmental standards.
Disc Granulator: High pelletizing rate (≥95%), uniform round ball shape, flexible visual control, ideal for 1-5 T/h commercial lines.
Rotary Drum Granulator: High throughput, heavy-duty continuous production, ideal for 5-20 T/h large industrial organic and bio-organic lines.
Double Roller Extrusion Granulator: Dry granulation requiring zero drying/cooling energy, ideal for powder blends with low moisture (10-15%) where thermal cost must be minimized.
Standard 1-5 T/h production lines are typically assembled, factory trial-run, and inspected within 25 - 35 working days after contract confirmation and drawing sign-off.
Large-scale 10-20 T/h custom automated plants require 40 - 55 working days. Complete factory trial run videos and QA inspection reports are provided prior to container loading.
For high-moisture organic waste (65%~85% moisture), we implement two proven industrial approaches:
1. Solid-Liquid Separation: Heavy-duty screw press or inclined screen separators reduce moisture to 50%~55% before fermentation.
2. Dry Material Blending: Mixing with dry carbonaceous materials (crushed straw, rice husks, sawdust, biochar) to adjust moisture to optimal 55%~60% for rapid aerobic fermentation.
Upon contract signing, we provide detailed "Civil Foundation Drawings & Plant Preparation SOPs" within 5 days. You will need to prepare:
1. Workshop building height (typically 6-8 meters clear height) and reinforced concrete floor;
2. Main 3-Phase power supply connected to the plant boundary transformer;
3. Heat source installation (biomass burner, natural gas, or steam) for the rotary dryer system;
Our engineers will arrive on-site to direct installation, belt conveyor positioning, electrical wiring, and test runs.
We support standard international trade terms (T/T wire transfer, irrevocable L/C at sight). All machinery is packed to maritime export standards: anti-rust oil coating for rotary cylinders, waterproof shrink film, and heavy-duty fumigation-free wooden crates for precision electrical cabinets, motors, and packaging scales.
Speak directly with our Chief Organic Fertilizer Equipment Engineer for free 1-on-1 consultation.
